RSD ChemSafe - B K Gopala Pumps and Equipments
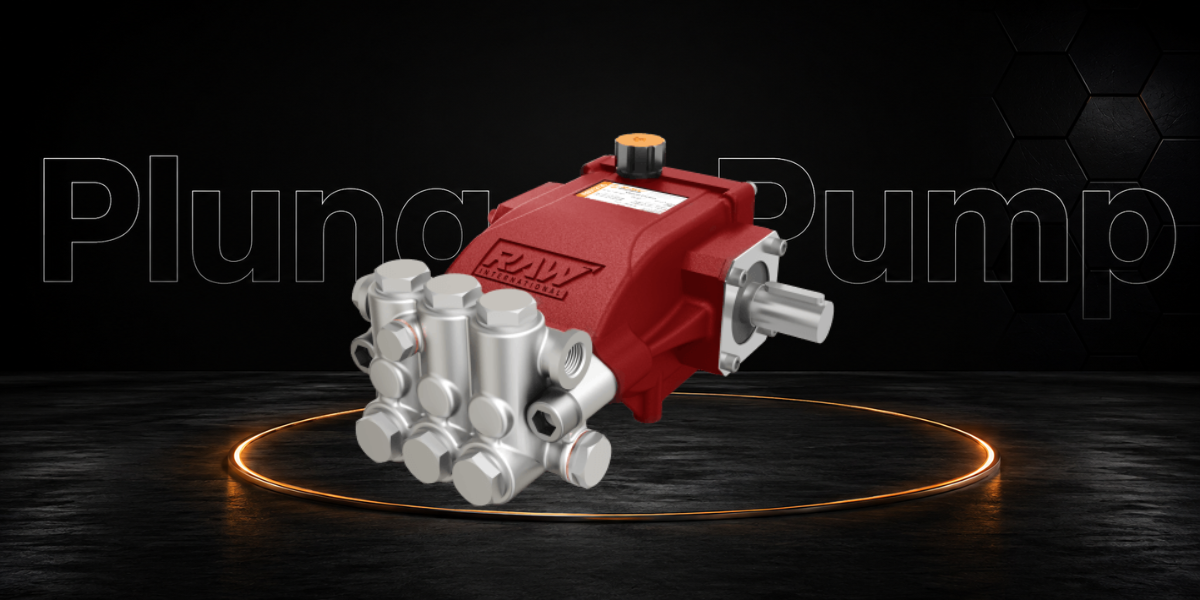
The RSD ChemSafe from B K Gopala Pumps and Equipments is an industrial pumping solution developed for applications where dependable fluid handling, controlled pressure, and reliable operation are essential. Designed with the requirements of challenging process environments in mind, this pump focuses on robust construction, consistent performance, and application-oriented engineering. Raw International is a renowned manufacturer specializing in the design and production of high-quality plunger pumps, offering professionally engineered solutions for industries that require reliable and efficient pumping technology.
The RSD ChemSafe is particularly suited to industrial operations where fluid characteristics require careful consideration during pump selection. Its application-focused design supports reliable handling of compatible process fluids while maintaining consistent pumping performance. The pump can be considered for demanding environments where equipment is expected to operate steadily over extended periods. Durable construction and a practical engineering approach help support dependable service, while correct material and configuration selection according to the process fluid can further enhance operational reliability.
A key advantage of the RSD ChemSafe is its suitability for a variety of process and chemical-related applications. Depending on the selected configuration, the pump can support operations involving compatible chemicals, industrial liquids, process fluids, water-based solutions, and other demanding fluid-handling requirements. Industries such as chemical processing, pharmaceuticals, manufacturing, water treatment, and general process industries can benefit from a purpose-oriented pumping solution. Factors including fluid composition, temperature, viscosity, pressure, flow rate, and installation conditions should be evaluated to determine the most suitable configuration for each application.
B K Gopala Pumps and Equipments emphasizes quality engineering and dependable manufacturing when developing industrial pumping equipment. The RSD ChemSafe is designed with attention to functional performance, construction quality, and long-term usability. Its engineering approach helps support stable operation while providing a practical solution for industries that need reliable pumping equipment in demanding process environments. Proper installation, periodic inspection, appropriate maintenance, and operation within recommended conditions are important for maintaining efficient performance and achieving a longer service life.
The RSD ChemSafe also represents the expertise of Raw International, a brand dedicated to manufacturing high-quality plunger pumps for industrial applications. With a focus on precision engineering, durable construction, and application-specific requirements, Raw International works toward delivering pumping solutions that address the practical needs of different industries. The RSD ChemSafe can be selected with consideration for the characteristics of the fluid and the demands of the process, helping customers develop a pumping system suited to their operating conditions. Professional technical assistance can further support appropriate pump selection and configuration.
Selecting the correct pump is important for maintaining process efficiency, protecting equipment, and ensuring consistent fluid movement. The RSD ChemSafe provides a reliable and professionally engineered option for industries requiring dependable pumping performance in chemically demanding and process-oriented environments. With the support of B K Gopala Pumps and Equipments, customers can evaluate their application requirements and identify an appropriate solution. Backed by the manufacturing expertise of Raw International, RSD ChemSafe reflects a commitment to quality, reliability, and practical industrial performance for modern fluid-handling applications.